 |
| April 03, 2018 | Volume 14 Issue 13 |
Mechanical News & Products
Designfax weekly eMagazine
Archives
Partners
Manufacturing Center
Product Spotlight
Modern Applications News
Metalworking Ideas For
Today's Job Shops
Tooling and Production
Strategies for large
metalworking plants
Siemens Meet at the Machine: Be productive from day one of new CNC machine delivery
 Traditionally, many programming, validation, and training activities begin only after a machine is installed. Not anymore. Meet at the Machine is Siemens' new initiative uniting machine builders, software, and automation for next-level CNC through a continuous digital thread across engineering, programming, virtual validation, and execution. By pairing a Digital Twin with Digital CNC powered by SINUMERIK, manufacturers can prepare, validate, train, and optimize workflows before your specialized machine's physical delivery! TRAK Machine Tools is the launch partner -- see what they are doing.
Learn more.
How to master metal powder management in 3D printing
 What's the real cost of "good enough" powder tracking for powder-bed fusion 3D-printing machines? According to Tim Wischeropp, CEO and Co-Founder of amsight, the technology is rife with hidden costs. Every cycle, every handling step, every exposure, and every mixing decision plays a part. Surprisingly, though, with the right strategy, users can turn their losses into a competitive edge. Learn how.
Read the full article.
Aluminum oxide filament for FDM printers
 Virtual Foundry, the company that brought us 3D-printable lunar regolith simulant, has a new product called Aluminum Oxide Filamet™, giving users the power to print alumina parts using the FDM printers they already own. This composite 3D-printing material allows researchers, engineers, and makers to bypass expensive ceramic tooling and produce pure ceramic components in-house. Print using a 0.6-mm hardened-steel, standard-flow nozzle on virtually any open-architecture printer.
Get all the material specs.
New metal extrusion retrofit system helps manufacturers get into ShAPE
 A new invention from the Department of Energy's Pacific Northwest National Laboratory could soon help manufacturers more easily adopt the lab's patented Shear Assisted Processing and Extrusion (ShAPE™) technology, enabling faster manufacturing of superior extrusion products while reducing costs and energy use.
Read the full article.
Pneumatics: Dual guide rod cylinders and exhaust silencers
 Automation-Direct has expanded its guided actuator lineup with compact 12-mm dual guide rod cylinders from Metal Work. Ideal for packaging and material handling, these double-acting cylinders feature 10-mm to 250-mm strokes, magnetic pistons, and integral sensor slots. Additionally, new durable acetal plastic silencers are now available in multiple NPT/BSPP sizes to reduce pneumatic exhaust noise.
Learn more.
Expanded injection molding capabilities
 Pexco LLC has acquired Recto Molded Products and Legacy Extrusions, expanding its capabilities in complex injection molding, tooling, assembly, and engineered thermoplastic solutions for OEM manufacturers. The Cincinnati-based companies bring more than a century of manufacturing expertise, advanced production technologies, and value-added services that strengthen Pexco's ability to support customers from product design through full-scale production. Injection molding presses ranging from 55 to 500 tons.
Learn about Pexco and its value-added manufacturing services.
Custom 3D-printed steering wheel for jet dragster
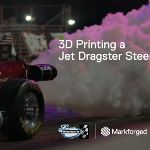 Jet dragsters use General Electric J85 engines -- the same turbines pulled from U.S. military F5 Freedom Fighters -- mounted to a custom 26-ft chassis. The racers achieve quarter-miles in 5.5 sec, but standard metal parts can fail custom ergonomic needs. Traditional manufacturing of low-volume aluminum steering wheels demands long, 8-day lead times, high costs, and multi-piece assemblies. Larsen Motorsports solved this by replacing metal with continuous fiber 3D printing using the Markforged X7. Embedding continuous carbon fiber into an Onyx nylon matrix allowed them to target specific load paths, delivering a custom steering wheel that is stiffer, lighter, and faster to produce than aluminum.
View the video.
Application Spotlight: Light-duty ring in an air vent nozzle
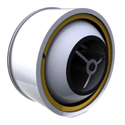 Explore how a light-duty Spirolox® retaining ring is used in an airplane air vent nozzle to regulate airflow. This application spotlight shows how the ring fits into a groove in the plastic housing, securing the nozzle during rotation. Designed for light loads and axial positioning, it offers a simple, economical solution that is easy to install and remove.
View this informative Smalley video.
Fasteners for automotive and agricultural equipment
 Norm Fasteners has acquired an automotive fastener manufacturing plant in Plymouth, MI, expanding its North American footprint beyond sales, engineering, and logistics. The local facility produces metric fasteners (M4-M24) and engine bolts. Norm’s portfolio includes wheel bolts, studs, custom fasteners, and licensed MAThread® and TAPTITE® products, serving diverse automotive and industrial assembly needs.
Learn more or contact Belgin Tunce
for more information.
3M Cooling Film for vehicle roofs launched
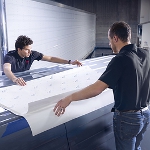 New 3M Cooling Film is a roof-applied heat-management solution designed to help keep vehicle cabins cooler, reduce cooling demand, and improve operational efficiency. The aftermarket product uses advanced thermal management technology to reflect more than 85% of solar radiation. Interior vehicle temperatures can be reduced by up to 10 degrees F with this product. Installs like graphics by professional installers using 3M adhesive technologies. Initially designed for fleet and rail operators.
Learn more.
Test your knowledge: High-temp adhesives
 Put your knowledge to the test by trying to answer these key questions on how to choose the right high-temperature-resistant adhesive. The technical experts from Master Bond cover critical information necessary for the selection process, including questions on glass transition temperature and service temperature range. Some of the answers may surprise even the savviest of engineers.
Take the quiz.
New Air Holster Safety Air Gun Mount
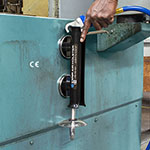 EXAIR's new Model 5930 Air Holster provides a simple and convenient way to keep Safety Air Guns secure and within easy reach at workstations throughout a facility. Designed to give operators a designated location for their air gun when not in use, the Air Holster helps prevent misplaced tools while keeping work areas organized and efficient. Its practical design makes it an ideal addition to manufacturing, assembly, maintenance, and other industrial workstations where Safety Air Guns are frequently used.
Learn more.
Southco access hardware in rail applications
 Discover how Southco's rail access hardware solutions help improve safety, reliability, and operational efficiency across modern rail networks. The video showcases a range of rail applications where Southco's access hardware plays a critical role, including driver cabins, lighting systems, tray tables, headrests, armrests, and other passenger and operator touchpoints. Designed to support dependable performance in demanding moving environments, Southco's solutions help operators streamline maintenance processes, minimize downtime, and enable more proactive asset management.
View the video.
Multi-zone tension leveler for hard-to-flatten alloys
 Redex USA's Levelflex® is a modular, multi-zone tension leveler engineered for continuous processing lines, including coating and heat treatment of aluminum alloys and where flatness is critical to coating adhesion and downstream formability. By stretching material within 95% of its yield strength, it corrects stubborn flatness defects in fewer passes. It comes in open-loop pure stretch or closed-loop tension measurement modes to optimize surface integrity and eliminate crossbow.
Learn more.
Hold any shape with ID and OD Form Holding Clamps
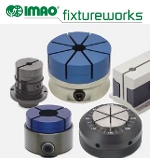 These simple OD and ID clamping solutions from Fixtureworks clamp onto your part in one easy operation, eliminating the need for custom fixtures. They allow users to clamp onto the inner or outer diameter of small-size, irregularly shaped work parts fast. Lots of options.
Learn more.
Researchers use 3D modeling to delve into what really happens with supersonic cold metal bonding
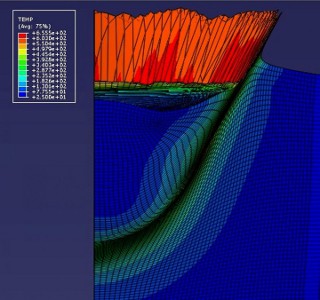
The Cold Gas Dynamic Spray (CGDS) process is very hard to predict. The CGDS deposition zone has now been 3D modeled to show the effects of temperature for the first time by Professor Tien-Chien Jen from the Univ. of Johannesburg. Here, the model predicts an orange/red "splash" of aluminum substrate just after a 5-micron copper particle has impacted it at 700 m/sec. [Credit: Hong-Shen Chen, Univ. of Johannesburg]
When a fragile surface requires a rock-hard, super-thin bonded metal coating, conventional manufacturing processes come up short. However, Cold Gas Dynamic Spray (CGDS) can do just that -- with a big caveat. CGDS is enormously versatile, but it is also very difficult to predict key aspects of the entire process. Now a temperature-based 3D model by Professor Tien-Chien Jen from the University of Johannesburg has started unlocking the mysteries of the CGDS film-growing process in the particle deposition zone.
The model is the first to connect the dots between particle impact velocity, energy transformation, and temperature rise in the particle impact zone, in three dimensions.
CGDS is already used extensively to manufacture or repair metal parts for large passenger airliners, as well as mobile technology and military equipment.
In the process, a de Laval nozzle sprays micron-sized metal particles over a short distance, typically 25 mm, at a metal or polymer surface. The particles impact the surface at speeds ranging from 300 m/sec to 800 m/sec. As a frame of reference, the speed of sound is 343 m/sec.
CGDS has the best temperature range of all industrial spraying processes in use today, and it saves energy, because no heating is added.
A manufacturing mystery
A mystery starts on the factory floor, however. If you have a 5-micron copper particle, how fast should it arrive at the deposition zone on aluminum, if you haven't used this combination before? Or you select a new metal for the particles, and a new metal for the surface: How do you even start guessing what size the particles should be, and at what speed they should impact the surface to give you a well-bonded coating?
Keep in mind, the CGDS-bonded coating should come without evaporation, crystallization, residual stresses, or other thermal damages -- some of the big reasons CGDS is used in the first place. These questions can have enormous financial implications for the manufacturing machines on the factory floor.
Physics still out
Why CGDS bonds metal particles to a substrate surface has defied understanding since its invention in the 1980s by the military, says Jen, Professor in the Department of Mechanical Engineering Science at the University of Johannesburg.
"At first, the military used CGDS to repair spare parts in the middle of nowhere. Then other industries realized you can use it on very fragile surfaces as well. You can create a new bonded surface only a few microns thick, or keep spraying until you have a 10-mm coating. Once you've filled in the cracks or holes, you can machine the part to have its exact dimensions again, because the GDS-bonded coating can be harder than the titanium or vanadium the part is made from."
The CGDS coating can be this hard because of the compressive stresses created when the particles impact the surface. The stresses increase the metal fatigue life, he says. This is similar to what happens in shot-peening, an industrial process similar to CGDS, but using "balls" a few millimeters in diameter to impact a surface.
"CGDS is used for very high-cost manufacture and repair, but there is no comprehensive, realistic model describing the physics of the entire process," says Jen.
3D with splashing
In CGDS, engineers talk about two zones. The first is the flight-zone between the spray nozzle and the surface to be sprayed. This zone was modeled by Jen in a 2005 research article in the International Journal of Heat and Mass Transfer.
The second zone is the deposition zone, where the sprayed articles impact the surface. The new 3D model describes this zone.
Previous two-dimensional models have attempted to solve the puzzle around CGDS bonding, but these have a severe limitation. When you extend a 2D model to 3D, you end up with a "horizontal cylinder" descending toward the surface being sprayed.
"Unfortunately, a descending cylinder cannot model realistically enough what happens to discrete ball-shaped particles 'splashing' down in the substrate surface," says Jen.
As industry knows, the speed (velocity) the particle arrives at the substrate is critical. Too slow, and it will just bounce off. Too fast, and it may pass like a bullet through a thin substrate.
The new model animates in 3D a single spherical particle "falling down" into the substrate metal. The substrate "splashes up," and then the particle and substrate bond. The substrate "splashing" looks like milk splashing up when something falls into the cat's bowl. This is called "jetting behavior" in industry, says Jen.
Cold metal, temperature rise
The model uses several parameters describing the nature of the particle and the surface: density, thermal conductivity, specific heat, melting point, elastic modulus, Poisson's ratio, Johnson-Cook plasticity, and Johnson-Cook damage.
It is the first to predict in 3D how the average temperature of the particle impact zone will rise and subside, depending on the size and impact velocity of the particle. The model was published in the Journal of Thermal Spray Technology.
Just fast enough to melt
"For this 3D model, we went with the hypothesis that a metal particle has to bond with the substrate at 60 percent of its melting temperature to create a strong new surface without damaging the substrate," says Professor Jen.
As an example, copper (Cu) has a melting temperature of 1,083 C, and 60 percent of that is 650 C. So the hypothesis says that a 5-micron copper particle impacting an aluminum substrate surface will have to be fast enough so that the average impact zone temperature goes up to at least 650 C, and not much more, for good bonding to occur. According to the model, that critical impact velocity range is between 700 and 800 m/sec.
Supersonic energy transformation
When a copper particle travels at a supersonic speed and hits an aluminum surface, its moving (kinetic) energy is converted into heat (thermal) energy, says Prof Jen. This depends on the impact speed of the particle.
"The heat makes the particle and the impact zone 'soft and sticky,' similar to melted cheese. The particle changes into a 'soft blob' that fills in the 'impact crater' in the substrate surface. At the same time, friction develops between the blob and the crater surface, which is critical to the bonding process," he says.
"The friction 'grabs' the blob, and it sinks into the substrate surface. As the blob sinks down, the molten substrate around the particle 'splashes up' in typical jetting behavior. When the jetting settles down, the bond between particle and surface is completed," says Jen.
Model vs. the real world
The model, though limited, holds up in experimental results with copper particles sprayed onto an aluminum surface.
"When the impact velocity is within the range predicted by the model for a particle size, sufficient bonding temperature is reached and a strong CGDS coating is created. As an example, we set up our CGDS equipment in the laboratory for copper particles with an average size of 5 micron, carried by nitrogen, and impact velocity in the range of 700 to 800 meters per second deposited downwards on aluminum.
"The model predicts that at about 750 meters per second impact velocity, the critical bonding temperature of 650 degrees Celsius will be attained in the particle impact zone. In line with that prediction, we obtained excellent CGDS bonded coatings," he says.
"However, as also predicted by the model, we found with our laboratory setup that when the particle impact velocity is not within the critical range, insufficient bonding temperature is reached. This can result in poor surface coating with loosened powders and scrapping surface, which don't meet manufacturing quality standards," says Jen.
Grand challenge remains
The single-particle single-layer 3D model will be extended into a multi-particle, multi-layer model in follow-up projects.
Says Jen: "This 3D model is the first to describe how the temperature of the impact zone influences particle deposition. However, realistically modeling the deposition zone in CGDS remains a grand challenge to solve. In real-world conditions, particles are not of uniform size or shape, and travel at different velocities and angles. So a more complete model will have to accommodate ranges, or distributions, of all of these parameters."
Source: University of Johannesburg
Published April 2018
Rate this article
View our terms of use and privacy policy